EXPERIMENT · 2024
ServoBrush
Problem
Bed levelling systems that use the nozzle to touch the bed need a clean nozzle. A bit of plastic on the tip and the probe reads wrong.
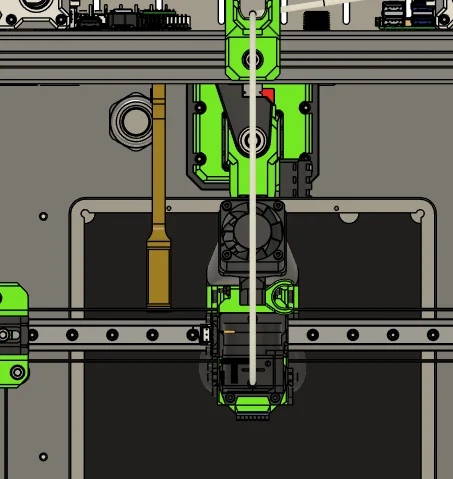
Most printers solve this with a brush parked past the edge of the bed. The V-core can't. It's tight on space. The nozzle never hangs over the bed edge, in any position. So a fixed brush would sit inside the print area and get run over. The brush had to move.
Process
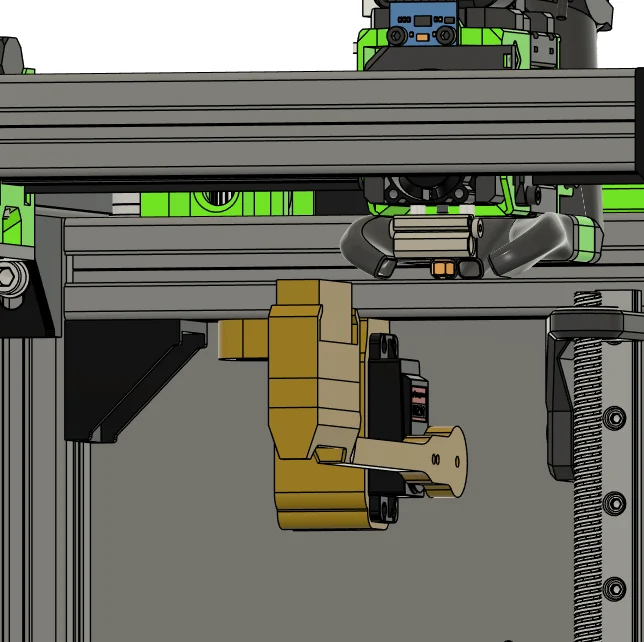
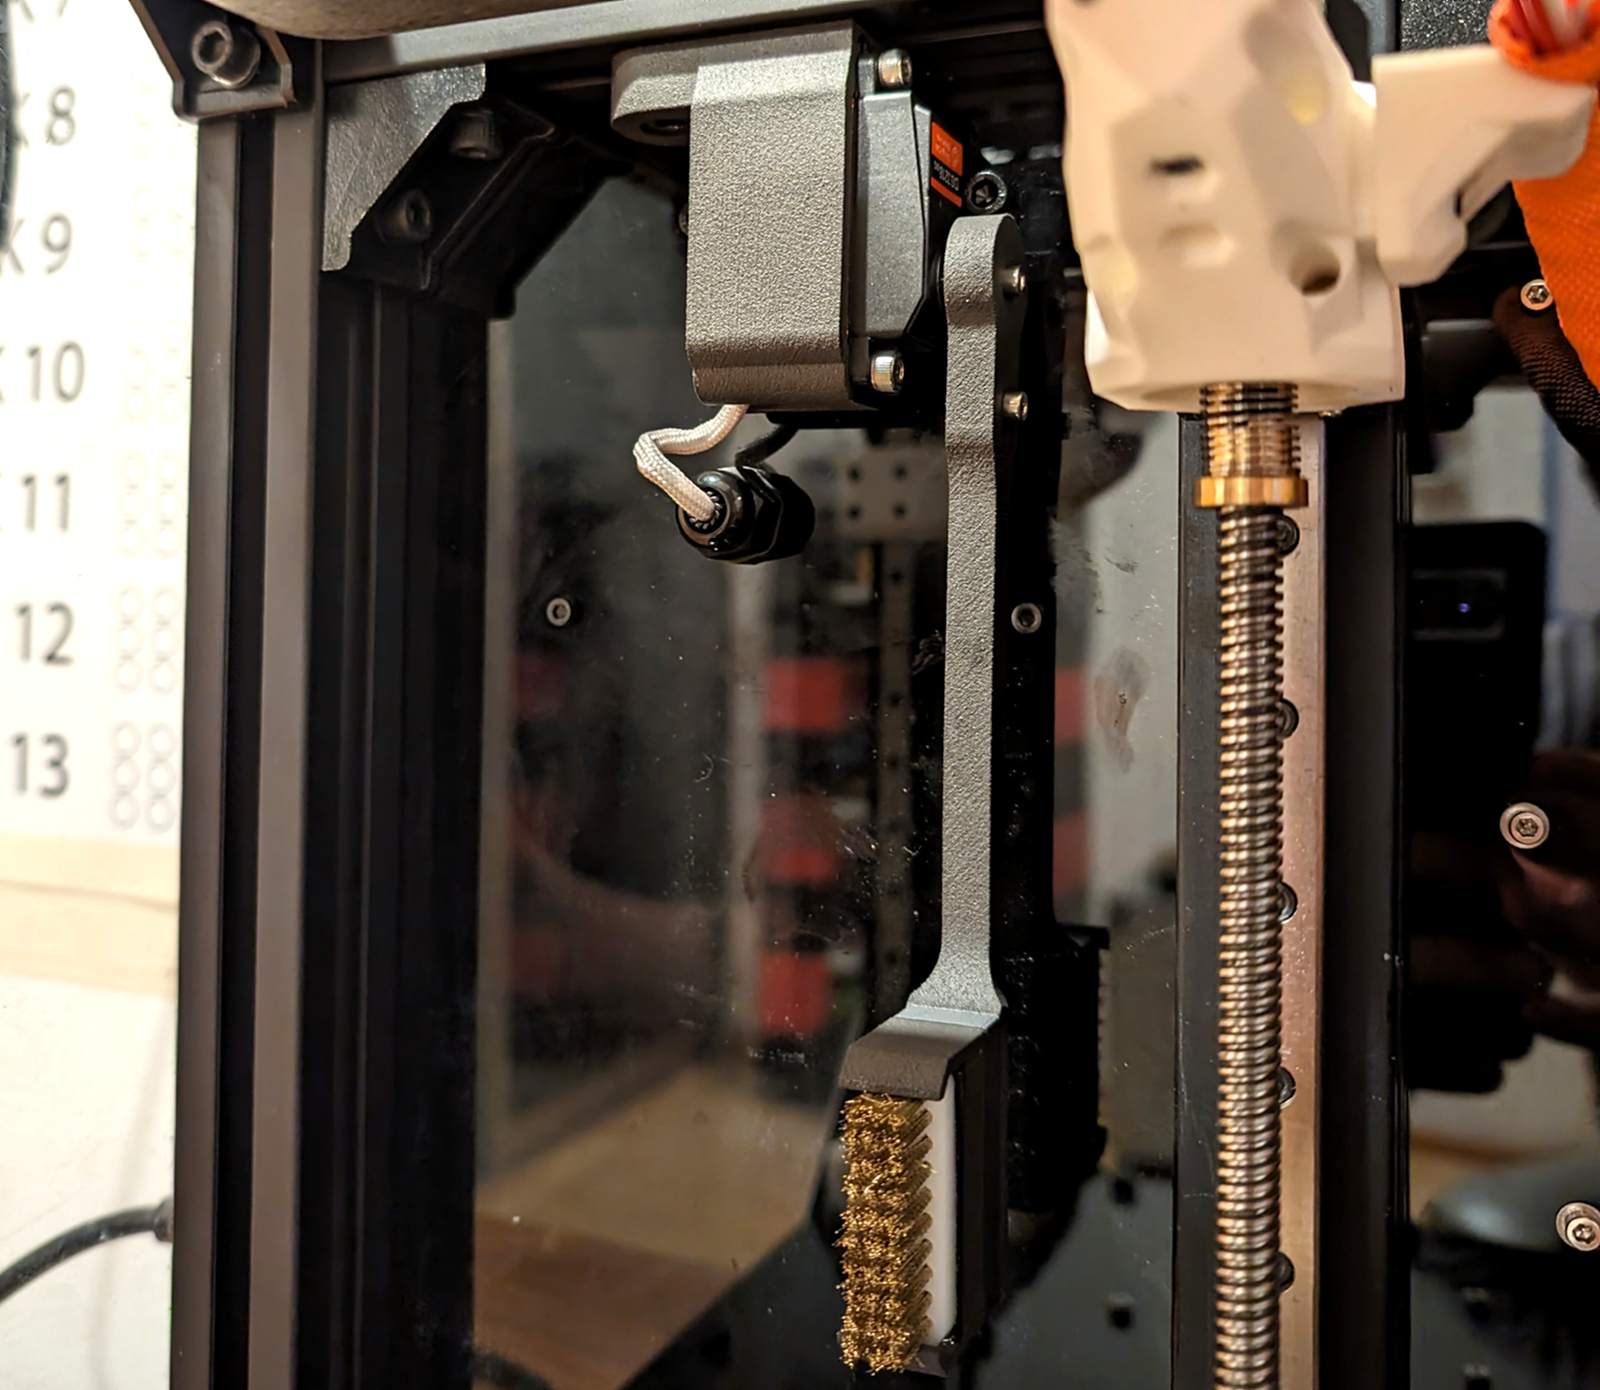
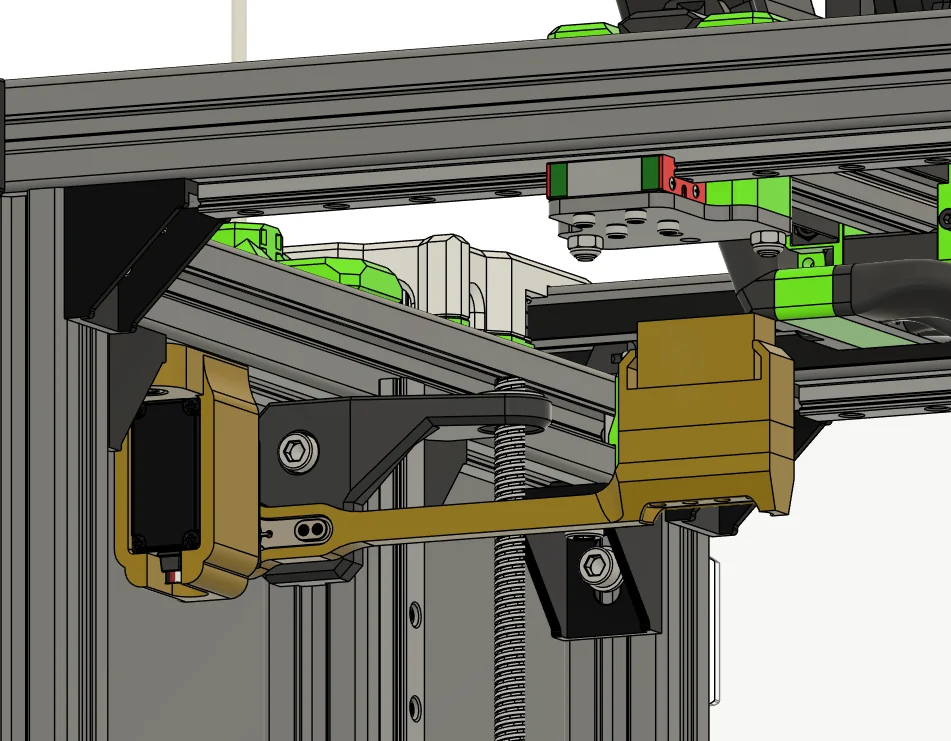
A servo swings the brush in when it's needed and out when it isn't. The servo bolts to a 3030 extrusion on the frame with two T-nuts. An arm reaches from the servo horn to a holder that takes a brass brush. Six printed parts, one servo, one brush.
Height was the fiddly bit. The brush has to touch the nozzle. Not miss it, and not shove it. So the height lives in its own spacer part. You scale that one part in the slicer until it's right. No CAD needed.
Then the Klipper macro. It drops the bed and heats the hotend to 200 C. It parks the toolhead over the brush and deploys the servo. Then it wipes. Side to side, front to back, then a circle each way.
The part I like is that the loop runs on temperature, not on a count. The macro sets the target back down to the preheat temp and turns the part fan on. Then it keeps wiping while the hotend cools. When it reaches the preheat temp the loop breaks, the servo stows, and the print carries on. So the wipe lasts exactly as long as the cooldown takes. And the plastic stays soft the whole way through.
There are 16 variables for the rest. Servo angles, speeds, park position, wipe distances, fan speed. There's also a verbose mode that narrates every step to the terminal and plays a sound.
The servo can go on the left or the right. So the arm is mirrored, and there are two files. A 270-degree servo is needed for the right side, because the arm has further to swing.
Outcome
It's on my printer and it still runs. Everything is public. Six STL files on Printables. The STEP file, the macro, and my variables on GitHub. My whole printer config is up there too. So you can see how it's actually wired, rather than guessing.
A few honest things. The parts were made for SLS, so on an FDM machine they need supports and come out rougher. The spacer works, but it means everyone has to tune their own brush height. A brass brush doesn't always get everything. A proper blob still needs a hand.
- PRINTER
- RatRig V-core 3.1
- SERVO
- 270 degrees · 20 kg · mounts left or right
- MOUNT
- 3030 extrusion · two M6 T-nuts
- PRINTED PARTS
- six · made for SLS · FDM needs supports
- MACRO
- Klipper · 16 variables
- STATUS
- open source
- STL FILES
- printables.com/model/913748